Johnson Service Bulletin SB-1189 - Modifying the 55 H.P. Test Propellers
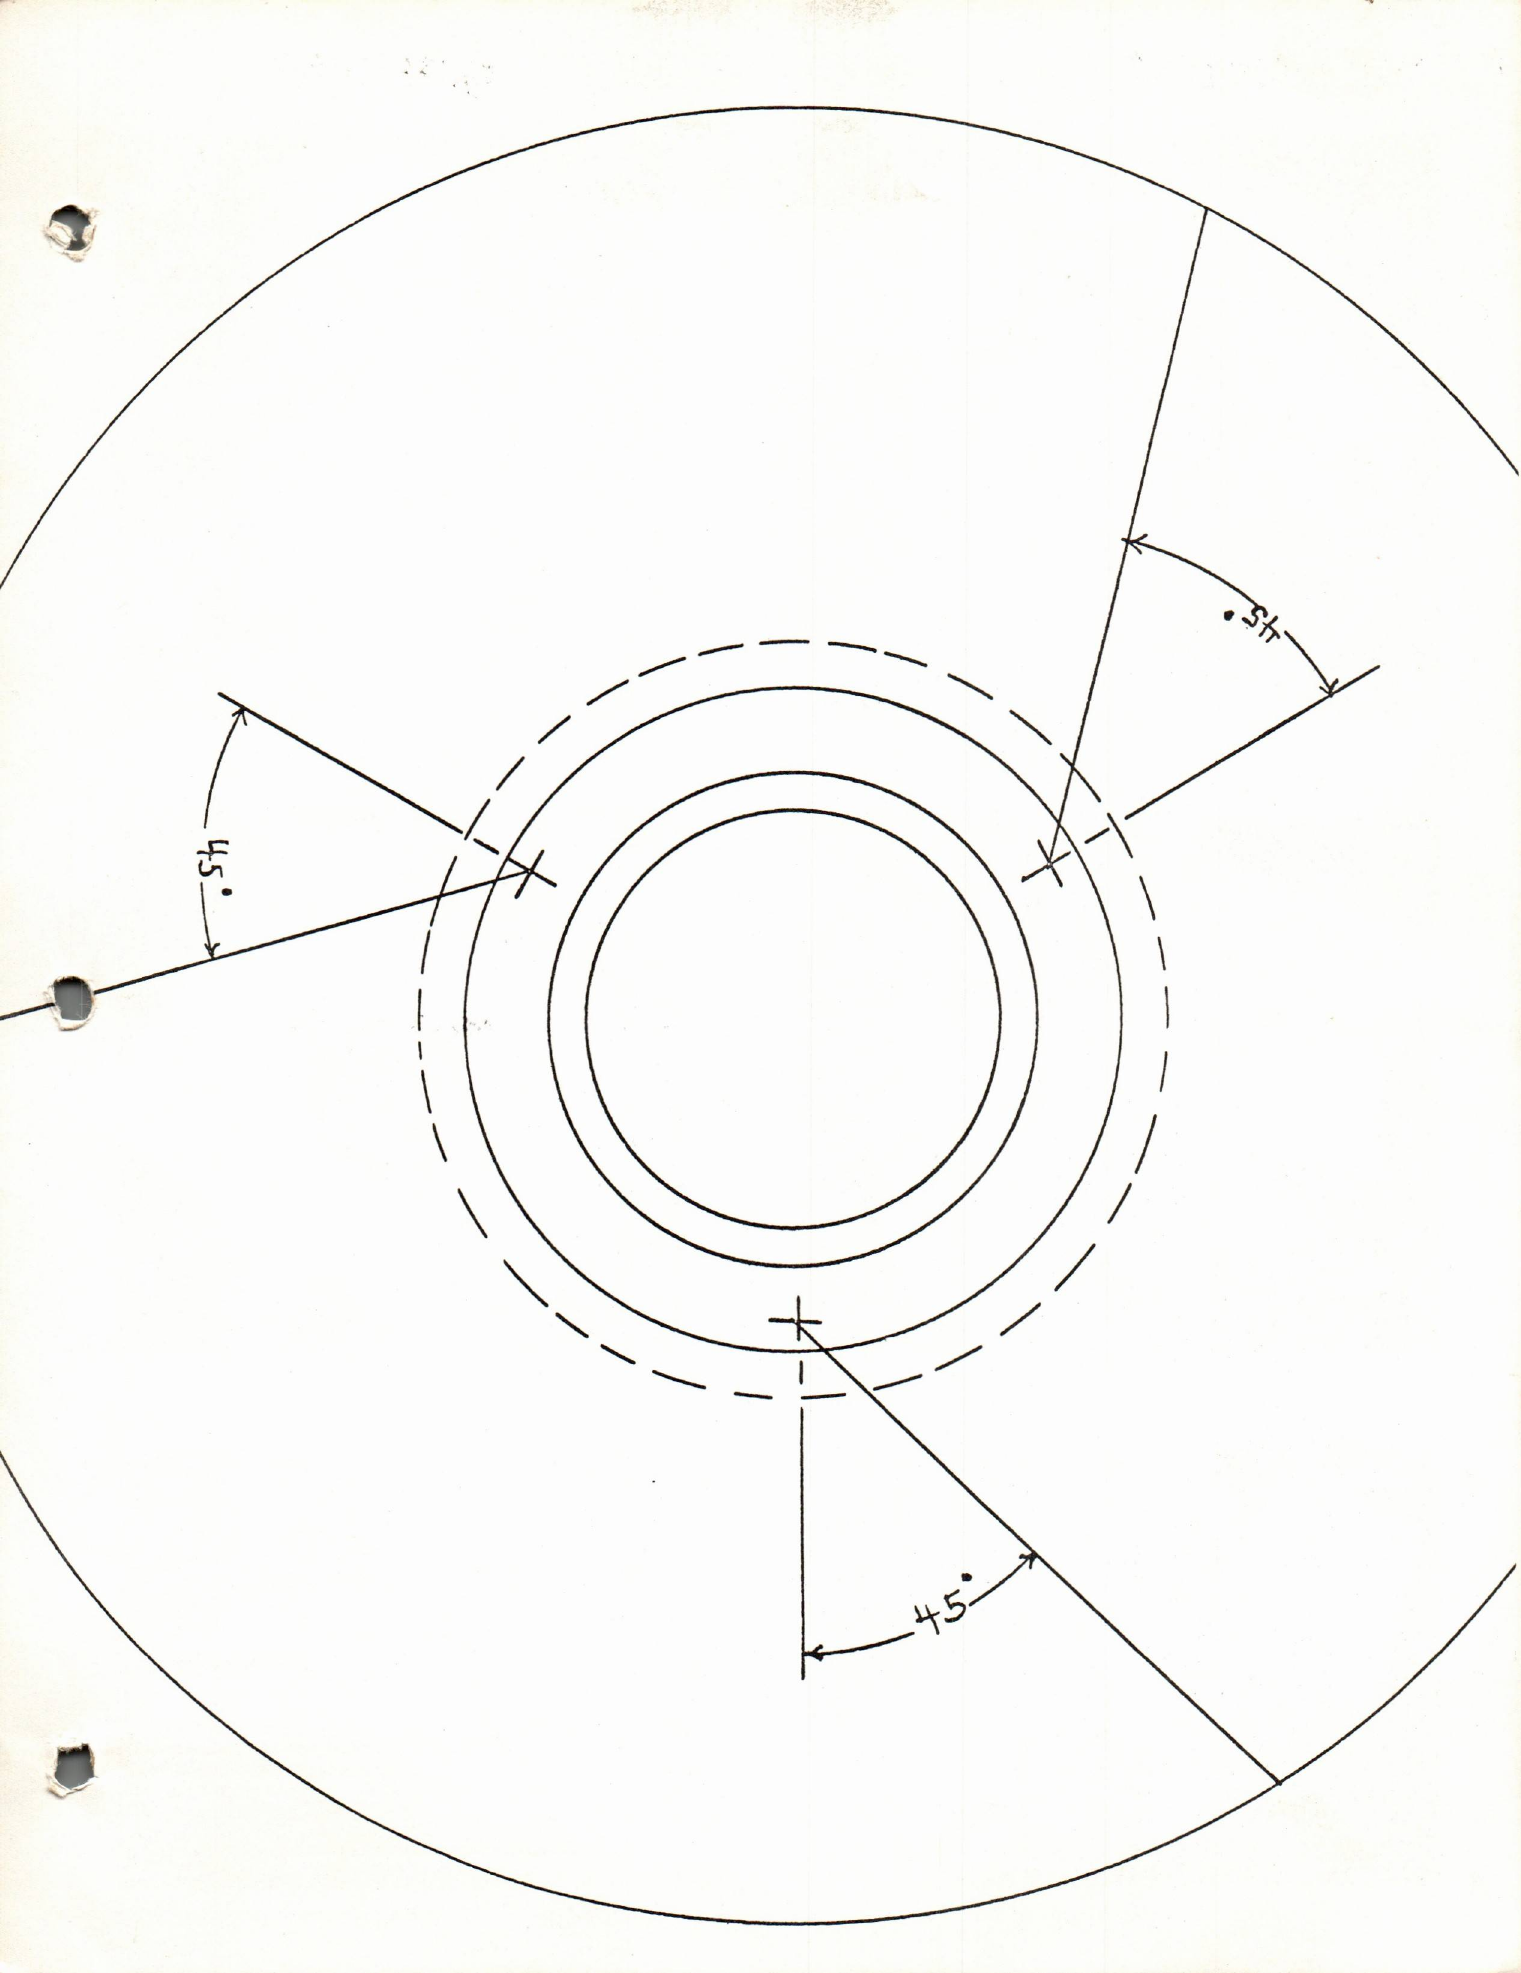
April 1969. Factory instructions for modifying earlier 55 H.P. test propellers to protect rear bearing seal 383120. The original drilling template is preserved as an image; check scale against the factory measurements before using it.

April, 1969
SUBJECT: MODIFYING THE 55 H.P. TEST PROPELLERS
ON MODEL: TR(L)-10, 55 H.P.
Changes have been made to the 55 H.P. test propellers to prevent possible damage to the Rear Bearing Seal #383120 on the 55 H.P. gearcases.
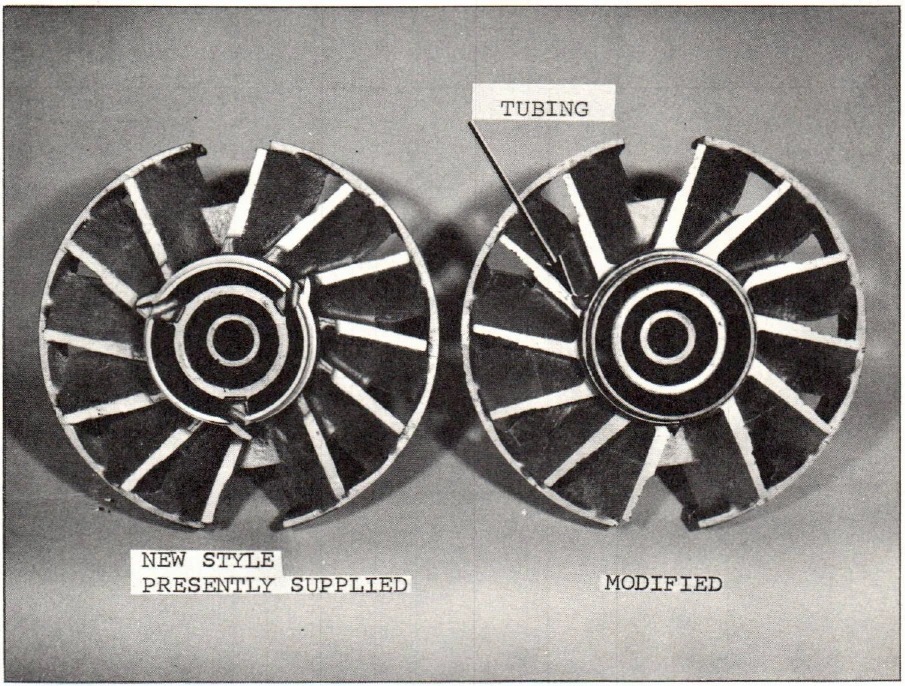
The following procedure should be followed in the event that you have one of the test propellers prior to the recent change. This involves drilling six holes and pressing in six pieces of copper tubing as shown in Figure 1.
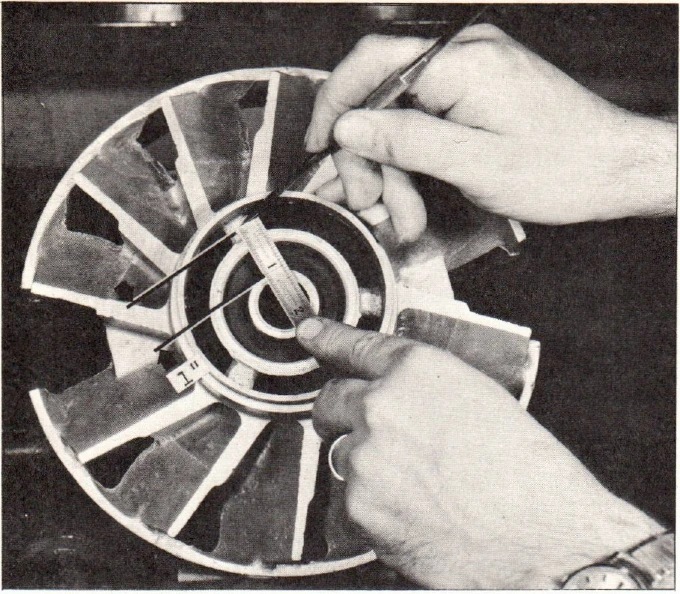
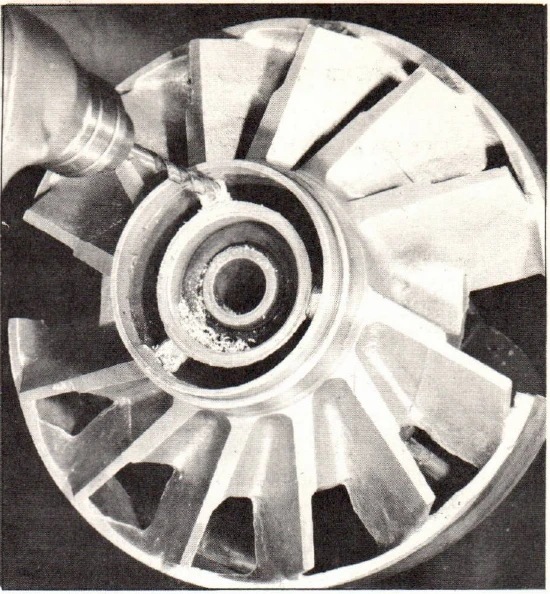
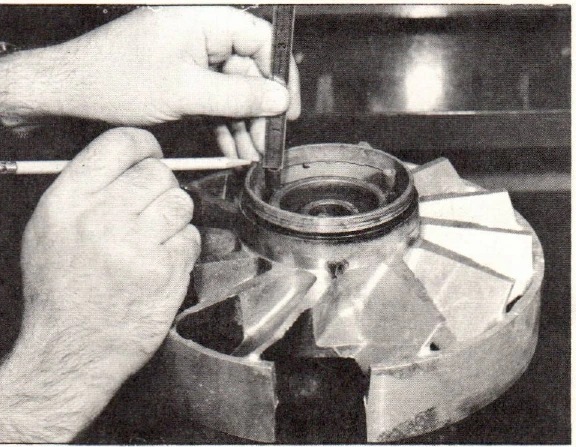
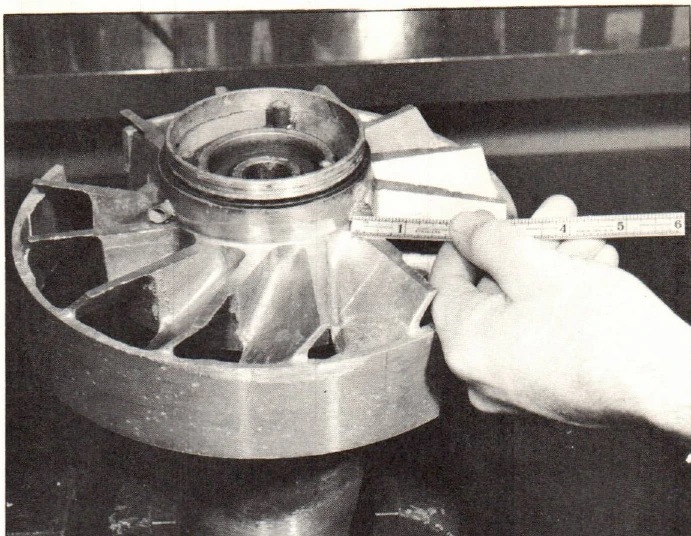
1. Measure 1" (one inch) on each web from the outer edge of the inner brass hub as shown in Figure 2. After scribing each web, take a 19/64" diameter bit, drilling 1-3/8" deep in each of the three webs as shown in Figure 3.
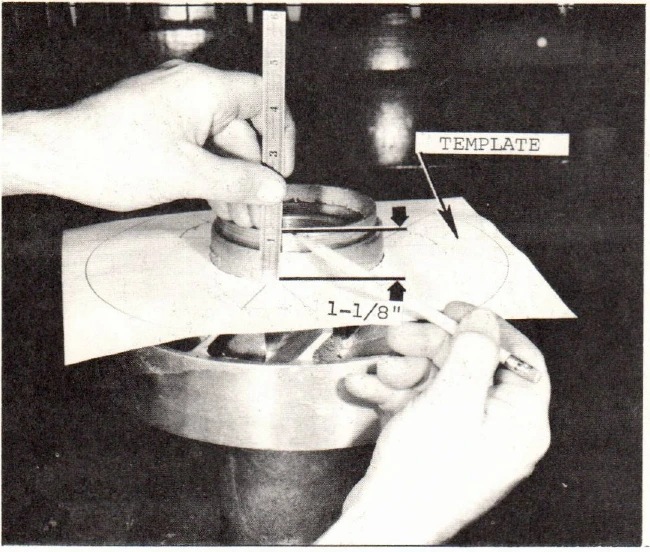
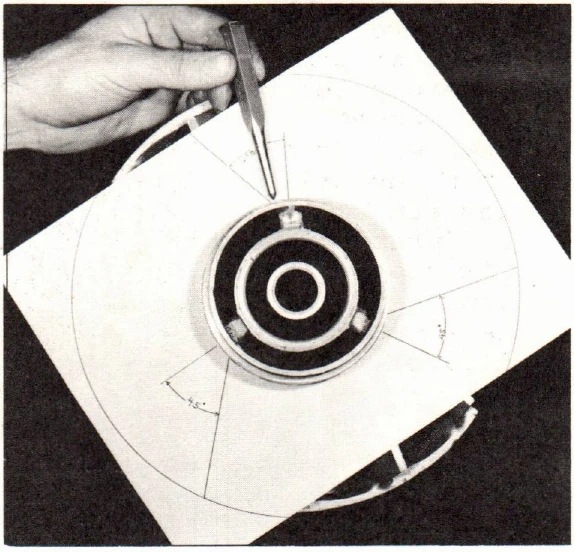
2. Take the attached template and cut along the dotted line. Lay the template over the test propeller as shown in Figure 4.
JOHNSON MOTORS, DIVISION OF OUTBOARD MARINE CORPORATION, WAUKEGAN, ILLINOIS 60085
JOHNSON MOTORS, DIVISION OF OUTBOARD MARINE CORPORATION, WAUKEGAN, ILLINOIS 60085
3. With the template lined up to the center of the three webs that join the outer hub to the inner hub, measure 1-1/8" from the top of the propeller as shown in Figure 4. Then center punch a mark where the 45° line meets the outer hub as shown in Figure 5.
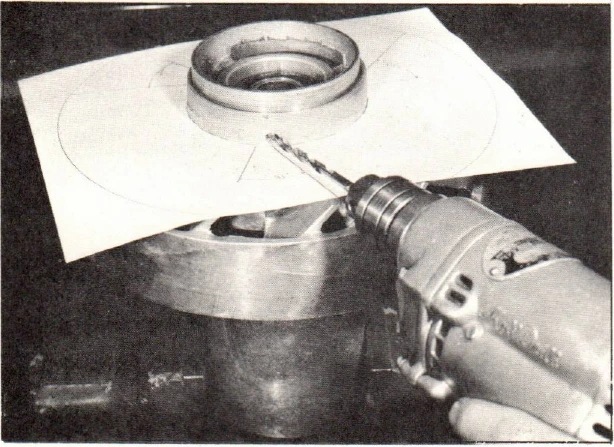
4. Drill the side hole at a 45° angle until it meets with the hole in the web as shown in Figure 6.
5. Cut three pieces of 5/16" copper tubing 3/4" long. Insert these in the webbing so the tubing be a measurement of 3/16" from the top of the outer hub as shown in Figure 7.
6. Cut three pieces of 5/16" copper tubing 7/8" long. Cut one end at a 30° angle. Insert these so they will protrude from the hub 7/16" as shown in Figure 8.
7. Using a center punch, stake each piece of tubing in place.
8. The test propeller on the right in Figure 1 is the modified 55 H.P. test propeller. The one on the left is the new style presently being supplied.
Doug Cankar
Administrative Assistant
DC:rkm
NOTE: Post on your TR - 55 H.P. Index under the heading "Miscellaneous."
Historical service reference
Applicable model: TR(L)-10, 55 H.P. Rear bearing seal: 383120. Factory drilling: 19/64-inch bit, 1-3/8-inch depth; 5/16-inch copper tubing. The full-size template is reproduced from the historical scan, but browser display and printing may alter its physical scale.